Trust In Quality With Us
Laser Cutting Machines
Showing all 5 results
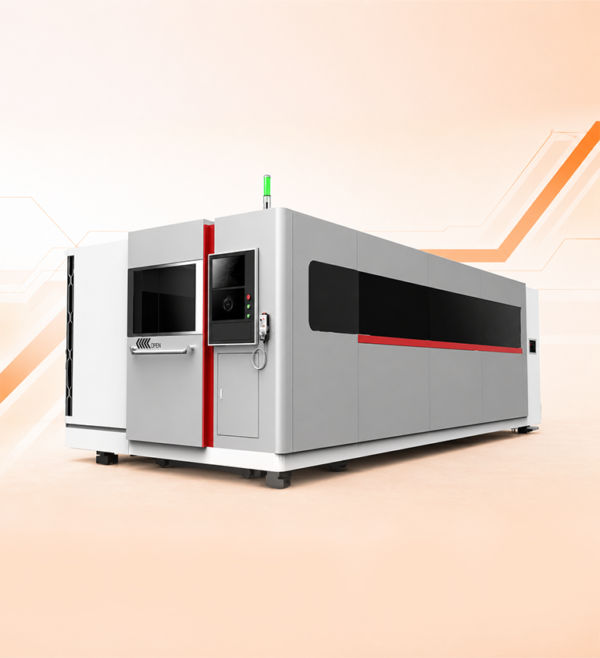
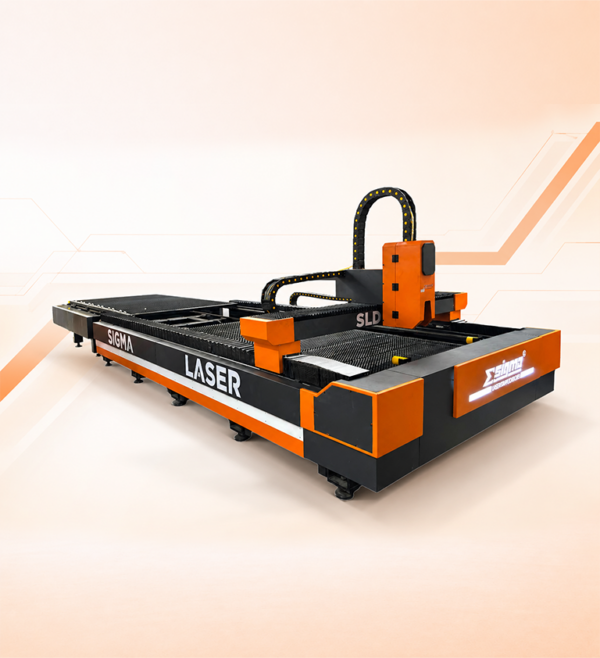
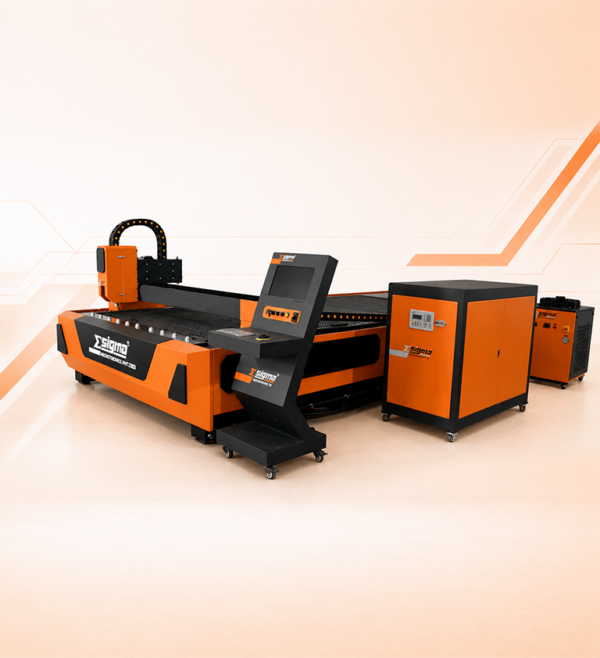
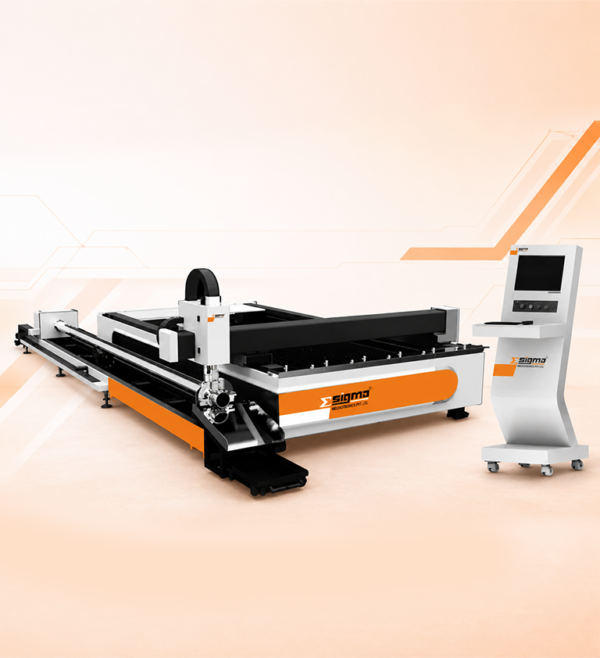
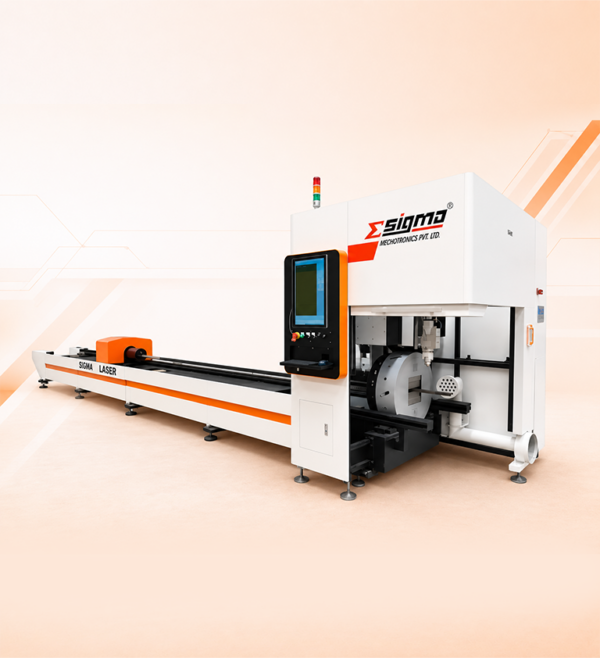
Laser Cutting Machines – Five Fiber Laser Configurations, 1.5 kW to 20 kW
A laser cutting machine is a CNC machine tool that cuts metal by focusing a laser beam to a spot a fraction of a millimetre across and blowing the molten material out of the cut with a jet of assist gas. Sigma Mechotronics Pvt. Ltd. manufactures fiber laser cutting machines in five configurations – open type single pallet, open type with auto pallet changer, close body, flat bed with a pipe and tube attachment, and a dedicated chuck-fed tube cutting machine. Flat-bed machines run 1.5 kW to 20 kW on six standard bed sizes from 3200 x 1600 mm to 6500 x 2500 mm, with custom beds built to a customer’s drawing; the tube machine runs 1.5 kW to 12 kW. This page is the decision page for the range: what separates the five, how to size the bed, how to select power, what the machine needs from your plant, and what actually sets the price.
- Power range
- 1.5kW-20kW
- Cutting configurations
- 5
- Largest standard bed
- 6500×2500 mm
- Standard bed sizes
- 6
Almost every buyer arrives at this category with the same three unresolved questions: how much laser power do I actually need, how big does the bed have to be, and what is this going to cost. The first two have answers, and they are answers your own work already contains – your thickest material, your largest part, your sheets per shift. The third one does not have a published answer, and any supplier who gives you a number before seeing those first two figures is quoting a machine, not quoting your machine.
The other question that gets asked too late is which body the machine should have. Power and bed size describe capability; the body – open with one bed, open with two beds and an automatic swap, or fully enclosed – describes how the machine will behave on your floor. It decides how stock is loaded, how much floor area the installation really occupies once the safety zone is drawn in, how the fume is handled, and how much of the shift the laser spends cutting rather than waiting for a sheet. Two shops with identical material and identical thickness can correctly buy different bodies.
Sigma Mechotronics Pvt. Ltd. manufactures these machines at its own plant in Ahmedabad, and the fiber cutting range came out of four years of dedicated development and a manufacturing facility built for it. Because the machine itself is designed and built there rather than imported and rebadged, a specification conversation is with the people who actually build it – including when the right answer is a bed size that is not in the standard list. This page is written for engineers, owners and purchase teams specifying a laser cutting machine for production: read it top to bottom and you should be able to write your own specification before you contact anyone.
At a Glance
Key Takeaways
The essentials, before the detail below.
Five Configurations, One Power Band
Single pallet, auto pallet changer, close body and flat bed with pipe attachment all run the same 1.5 kW to 20 kW fiber sources. The dedicated tube machine runs 1.5 kW to 12 kW.
Body Type Is a Floor Decision
Power and bed size come from your work. The body – open, open with two pallets, or enclosed – comes from your building, your material handling and who else works near the machine.
Six Standard Beds, Plus Custom
3200×1600, 4000×2000, 6000×2000, 6300×2000, 6500×2000 and 6500×2500 mm across every flat-bed configuration, with custom bed sizes manufactured to a customer’s drawing.
Sheet, Tube, or Both
A rotary attachment on a flat bed handles occasional 3 m and 6 m tube work. A dedicated chuck-fed machine handles tube as the business, including C, H, L and I profiles and +/-45 degree bevel.
The Bed Is the One Fixed Decision
Power can be discussed, options can be added, peripherals can be upgraded. The working envelope is set at manufacture and stays that size for the life of the machine.
Fiber Cuts Metal, Not Plastic
These machines cut mild and carbon steel, stainless and aluminium as standard, plus titanium, brass and copper with a reflective-rated head. Acrylic, wood and rubber need a CO2 laser instead.
Utilities Are Part of the Specification
Connected load, chiller duty, assist gas supply and fume extraction all scale with the source you choose. Plan them with the machine, not after it lands.
Built and Supported in India
Manufactured at our own Ahmedabad plant, ISO 9001:2015 certified, MSME and GST registered, with a 2-year warranty on manufacturing defects and critical spares held in India.
The Range
The Five Laser Cutting Machine Configurations We Manufacture
Every machine here is a fiber laser machine and they share the same cutting process, the same materials and – across the flat beds – the same six standard bed sizes. What separates them is body, automation and the stock format each one is built to hold. Start here, then use the sections below to fix the numbers.
| Configuration | Body, Automation & Stock Format | Built For |
|---|---|---|
| Single Pallet – Open Type | Open on all sides, one bed, manual load and unload. Flat sheet and plate. 1.5-20 kW. | Mixed job work where sheet size and thickness change daily, crane-loaded plate and awkward off-cuts. Mechanically the simplest machine in the range. |
| Auto Pallet Changer – Open Type | Open type, two working beds with an automatic swap mechanism. Flat sheet and plate. 1.5-20 kW. | Repeat-batch and volume production. One pallet is loaded while the other is cutting, so loading stops competing with cutting for the shift. |
| Close Body | Fully enclosed cabin with interlocked access doors and integrated dust and fume extraction. Flat sheet and plate. 1.5-20 kW. | Shared or occupied floors where beam containment, fume containment and a quieter working area are the priority rather than open crane access. |
| Flat Bed + Pipe/Tube Attachment | Flat bed with a rotary tube attachment. Sheet plus round, square and rectangular tube in 3 m and 6 m lengths. 1.5-20 kW. | Shops that are mainly sheet but take regular railing, frame or handle work, and cannot justify the floor space or capital of a second machine. |
| Dedicated Tube Cutting | Chuck-fed with automatic lubrication, two chuck models covering 20 to 350 dia., 3 m and 6 m stock, +/-45 degree bevel. 1.5-12 kW. | Tube, pipe and profile as the business – including C, H, L and I open channels and special sections. This machine does not cut flat sheet. |
How to read this table – the three flat-bed bodies are not a good, better, best ladder and they are not priced as one. They are three answers to a different question: how does material get on and off the bed, and what has to be contained. A job shop with a crane and varied stock is usually right to buy the simplest open machine even when it can afford the pallet changer, and a fabricator running the same nest all week is usually wrong to save money on one. Tell us your sheets per shift and your programme lengths and we will work the arithmetic with you before you commit.
Deciding Between a Pipe Attachment and a Tube Machine
This is the comparison buyers most often get wrong, because both options appear on a specification sheet as “cuts tube”. The attachment is a rotary axis added to a flat-bed machine: the sheet capability is unchanged, tube is handled in round, square and rectangular sections at 3 m and 6 m, and the machine goes back to sheet work when the tube job is finished. What it does not offer is bevel cutting, open profile sections such as C, H, L and I, or the chuck-and-clamp feed built for throughput.
The dedicated machine grips and rotates the section under the head through two chuck models covering 20 to 350 dia., cuts +/-45 degree bevels for weld preparation directly off the machine, handles open channel and special profiles, and has automatic lubrication on the feed system because it is expected to run tube continuously. The honest test is volume and edge requirement: occasional tube alongside sheet work is an attachment, tube as a product line with welded joints is a dedicated machine. Buying the attachment for a tube business costs you the throughput; buying the tube machine for a sheet business leaves you without a sheet cutter.
Definition
What Is a Laser Cutting Machine?
A laser cutting machine is a CNC machine tool that cuts material by focusing a high-power laser beam onto the workpiece, melting a narrow line through it, and clearing the melt with a coaxial jet of assist gas. On a flat-bed machine the sheet or plate lies on a slatted bed and the cutting head travels over it on a CNC-controlled gantry; on a tube machine, chucks grip and rotate the section under the head instead. Because the beam is the tool, there is no punch, no die and no tool change – the part geometry is a program, and a new part is a new file rather than new tooling.
The assist gas is not a detail. Cutting mild steel with oxygen sets off an exothermic reaction in the kerf that contributes its own heat, which is why oxygen is the fastest and most economical gas on carbon steel and why the resulting edge carries an oxide layer. Nitrogen does no such thing – it simply blows the melt out under pressure and shields the cut, leaving a bright, oxide-free edge that can be welded or painted without further preparation, at a much higher gas cost. Compressed air sits between the two and suits thinner gauge work where a light oxide on the edge is acceptable. Choosing the gas is choosing between edge quality and running cost, and it is decided per material, not once for the machine.
Every cutting machine in this range uses a fiber laser source rather than CO2. The practical differences are settled ones: a fiber source emits at around 1064 nm against 10,600 nm for CO2, so the beam is delivered to the head through a fiber cable rather than a mirror path that needs alignment, and it focuses to a much smaller spot. Wall-plug efficiency sits in the region of 20 to 30 percent for fiber against roughly 5 to 10 percent for CO2, which shows up directly on the electricity bill over a machine’s life. The shorter wavelength is also absorbed far better by metals, including reflective ones such as brass, copper and aluminium, where CO2 struggles. There is no laser gas mixture to buy and no resonator optics to realign. For production metal cutting, this is why fiber has replaced CO2 rather than sitting alongside it.
Fiber Laser, CO2, Plasma or Waterjet – Which Process Your Work Actually Needs
| Process | What It Is Genuinely Best At | The Trade-off You Accept |
|---|---|---|
| Fiber laser | Sheet and plate in mild steel, stainless and aluminium with a narrow kerf, a square edge and a small heat-affected zone; fastest of the four on thin to medium gauge, and the only one of them that also does fine detail, small holes and text | It is a metal process. Highest capital cost of the four, which is only recovered where cutting volume is real |
| CO2 laser | Non-metals – acrylic, wood, MDF, paper, fabric, leather and many plastics, which fiber cannot cut | Roughly 5-10 percent wall-plug efficiency, a mirror beam path to maintain and laser gas to buy; no longer the economical choice for production metal cutting |
| Plasma | Thick carbon steel plate at a low cost per cut, on a machine that costs a fraction of a laser | A far wider kerf, more heat into the part, edge taper and dross – so parts needing a precise or weld-ready edge go on to a secondary operation |
| Waterjet | Anything at all – metal, stone, glass, composite, heat-sensitive alloys – with no heat-affected zone whatsoever | Slow compared with a laser on sheet metal, and abrasive plus consumable cost per cut is high |
Say this out loud before you order – a fiber laser is a metal cutting machine. It will not cut acrylic, wood, MDF, rubber, foam, glass or stone, and no amount of power changes that – the wavelength is simply not absorbed the way those materials need. If a genuine part of your work is non-metal, plan a separate process for it. A machine bought on the assumption that it will cover both ends up doing one of them badly.
What a Fiber Laser Cutting Machine Changes on the Floor
01
No Tooling, No Tool Change
A new part is a new program. There is no punch or die to make, store, sharpen or wait for, which is what makes small batches and one-off jobs viable.
02
Any Geometry in One Setup
Outer profile, internal cutouts, holes, slots and engraved text are all cut in the same pass from the same file, with no repositioning and no second machine.
03
Narrow Kerf, Small Heat Zone
A kerf measured in tenths of a millimetre lets parts nest close together, and the small heat-affected zone means less distortion to correct afterwards.
04
No Cutting Force on the Part
Nothing touches the material, so there is no tool wear, no mechanical distortion and no clamping force to design a fixture around.
Where It Fits
Matching the Configuration to How Your Shop Actually Runs
The specification that fits is the one that matches your material flow, not the one with the most features. Find your work profile below, then confirm the bed size and power in the two sections that follow.
| Your Work Profile | The Configuration That Suits It, and Why |
|---|---|
| General job work – sheet size, thickness and material change from job to job | Open type single pallet. Nothing encloses the bed, so unpredictable stock, full plate and remnants all load from overhead without a door opening deciding what fits. |
| Repeat batches, many sheet changes per shift, cost per part is the measure | Auto pallet changer. Loading and unloading happen on the second pallet in parallel with cutting, so idle time between sheets stops eating the shift. |
| Shared floor, staff working nearby, coated or galvanised stock in the mix | Close body. The enclosure with interlocked doors contains the beam, and integrated dust and fume extraction handles what the material gives off at source. |
| Mostly sheet, with regular railing, frame, furniture or handle work in tube | Flat bed with pipe and tube attachment. One machine, one floor position and one operator covers both, at 3 m and 6 m tube lengths. |
| Tube, pipe and structural profile is the product, with welded joints | Dedicated tube cutting machine. Chuck feeding, open profile handling and +/-45 degree bevel produce weld-ready ends straight off the machine. |
| Thick structural plate at volume | Any flat-bed body, specified at the top of the power band. Here the decision is power and bed size first; the body follows from your loading method. |
| First laser in the shop, no laser experience on the team yet | Open type single pallet, or close body if the floor is shared. Fewest systems to learn, and the most forgiving machine to place while the team builds experience. |
One constraint worth knowing early – body type does not limit laser power on the flat-bed machines. All three bodies and the pipe attachment version are available across the full 1.5 kW to 20 kW range, so you never have to trade the body you need against the power you need. The single exception is the dedicated tube machine, which runs 1.5 kW to 12 kW.
Standard & Custom
Bed Sizes: Six Standard Options Across the Flat-Bed Range
The same six standard beds are available on the single pallet, auto pallet changer, close body and pipe attachment machines, and custom beds are manufactured to a customer’s drawing. This is the specification most often decided wrongly, because buyers size for the job they run every day rather than the largest job they need to be able to accept.
| Bed Size (mm) | Typically Suits | What to Weigh Before Choosing It |
|---|---|---|
| 3200 x 1600 | Panel, enclosure and signage work, precision job shops, buildings with a genuinely tight bay | The compact option, and the only one that comfortably fits a proper safety zone into a small bay. It takes the widely used 3000 x 1500 mm plate format with margin to spare. |
| 4000 x 2000 | General sheet metal fabrication – the all-round choice for most Indian job shops | Takes standard 4 ft x 8 ft sheet comfortably. If you cannot name a specific job that needs more, this is usually the size that stops you paying for capacity and floor area you never use. |
| 6000 x 2000 | Long structural parts, ducting, chassis rails, larger panel work | The entry point into 6 metre work, for shops whose length requirement runs well ahead of their width requirement. Check the crane travel covers the full bed before you commit. |
| 6300 x 2000 | 6 metre stock where end clamping or nesting margin is tight | The extra 300 mm is working margin rather than extra part capacity. Specify it when your parts genuinely run the full 6 metres and you keep losing the last one in the nest. |
| 6500 x 2000 | Long-format work with a generous nesting allowance | More length again at the same 2000 mm width. Chosen where sheet is fed long and nested tightly, and where scrap percentage is a number the shop actually tracks. |
| 6500 x 2500 | Heavy fabrication, wide plate, the largest work in the standard range | The maximum standard bed. Worth it only where the width requirement genuinely exceeds 2000 mm – the extra width costs floor area on all four sides and needs the crane access to match. |
How to read a bed dimension – it is the machine’s working envelope, not a sheet size. Your usable cutting area is the bed minus the clamping, edge margin and nesting allowance your parts need, so a 4000 x 2000 mm bed does not mean 4000 x 2000 mm of part. Size against the largest job you would want to accept over the next few years rather than the ones on the floor today. Power can be discussed and options can be added later; the bed is fixed at manufacture and stays that size for the machine’s whole life.
When a Custom Bed Is the Right Answer
Where none of the six standard beds suits the work or the building, we manufacture the machine to a customer-specified bed size. This is a build-to-drawing job rather than a catalogue variant, so the specification is agreed in engineering before manufacture starts. It is genuinely warranted in four situations: your part length or width sits between two standard sizes and stepping up buys capacity you will never use; the building rather than the work sets the limit, because bay width, column spacing, shutter opening or crane path rules out a standard footprint; the machine has to drop into an existing line where racking, a press brake or material flow dictates the geometry; or you cut one dominant blank format at volume, where a bed sized around that format saves nesting waste on every single sheet for years.
Send us your largest and smallest regular part dimensions, your typical incoming sheet or plate size, your material and thickness range, and a shop-floor drawing showing available space including crane access and room for the safety zone. That is enough for our engineering team to tell you honestly whether a standard bed already covers you – which it often does – or whether a custom build is worth the engineering.
1.5 kW to 20 kW
How to Select Laser Power
Power is decided by three things: the thickest material you must cut, the thickness you cut in the highest volume, and the cutting speed the second of those has to run at. It is not decided by bed size, not by body type and not by budget. The full 1.5 kW to 20 kW band is available on all four flat-bed configurations; the dedicated tube machine runs 1.5 kW to 12 kW.
| Power Band | Generally Suits | Where It Runs Out |
|---|---|---|
| 1.5 kW – 3 kW | Thin to medium gauge sheet, panel, enclosure and signage work, precision parts, lower-volume job shops | Thick plate, and any job where cycle time on medium plate is already the bottleneck rather than the machine’s availability |
| 4 kW – 8 kW | The broad production middle – mixed sheet and medium plate at commercial speed, and where nitrogen cutting on stainless has to stay fast | Heavy structural plate at high throughput, where the cut time per part stops being competitive |
| 10 kW – 20 kW | Thick plate, structural steel and high-speed thick-section cutting at volume, and shops selling capacity on thickness other machines cannot reach | Nothing capability-wise. The limit is capital and running cost, so specify it where thickness or throughput genuinely demands it |
Two things about power are worth understanding before you compare quotations. The first is that the return on extra power is not linear across thicknesses. On thick plate, more power converts almost directly into cut speed and into thickness capability. On thin gauge it does not – past a certain point the limit is the machine’s acceleration, the corner handling and the gas dynamics rather than the source, so a shop cutting mostly 2 mm sheet gains far less from doubling the source than a shop cutting mostly 16 mm plate. Specifying to your dominant thickness is how you avoid paying for capability that your parts cannot use.
The second is that the source sets the size of everything around it. Connected electrical load, chiller and cooling capacity, assist gas consumption and supply arrangement, and extraction sizing all scale with the laser you choose. A source specified without checking those is a source that arrives before the plant is ready for it. Our engineering team works through those points with you before quoting, so the machine that ships suits the building it has to run in.
Expert note on gas and reflective metals – oxygen gives the most economical and fastest cut on mild steel and leaves an oxide edge, nitrogen gives a clean weld-ready edge on stainless and aluminium at a much higher gas cost, and compressed air suits thinner gauge where light edge oxide is acceptable. Nitrogen consumption is the running cost that scales fastest with power and thickness – at the top of the power band on thick stainless it can outweigh electricity, which is why high-volume nitrogen users evaluate a generator or bulk supply rather than cylinders. Aluminium, brass and copper are highly reflective at the fiber wavelength, so confirm the cutting head is back-reflection protected before running them regularly, and tell us at specification stage if they are in your material mix.
What It Cuts
Materials, Assist Gas and What Each One Demands
Across the range these machines cut mild and carbon steel, stainless steel and aluminium sheet and plate as standard, with titanium, brass and copper cut where the head is rated for reflective material. Each material brings its own gas choice and its own thing to watch.
| Material | Usual Assist Gas | What to Watch |
|---|---|---|
| Mild and carbon steel | Oxygen; air or nitrogen on thin gauge | Oxygen is the cheapest and fastest route on plate, but the edge carries an oxide layer – specify nitrogen where the part is painted or welded straight off the machine. |
| Stainless steel | Nitrogen | Gives a bright, oxide-free, weld-ready edge with no secondary preparation. Nitrogen volume is the running cost that scales fastest with thickness and power – budget it properly. |
| Aluminium | Nitrogen | Reflective and highly thermally conductive, so it needs more power per millimetre than steel and a back-reflection protected head. Dross on the underside is the usual quality complaint. |
| Brass and copper | Nitrogen | The most reflective of the common metals. Back-reflection protection on the head is not optional here – tell us before you order if these are in your regular mix. |
| Titanium | Nitrogen or argon | Reactive at cutting temperature, so inert shielding governs edge quality. Confirm the grade and thickness with us rather than assuming steel parameters transfer. |
| Galvanised, coated and painted stock | Depends on gauge and finish | It cuts, but the fume is the real issue. Extraction has to be sized for this material rather than for bare steel, and this is where a close body machine with integrated extraction earns its cost. |
Indicative Cutting Thickness by Power Band
The table below gives the thickness ranges generally achieved by fiber laser cutting at each power band across the industry, using the usual assist gas for each material. Treat it as a sizing reference for narrowing your power band before you enquire – not as a performance guarantee. Actual capability on your work depends on material grade, gas purity and pressure, nozzle and focus setup, plate flatness and, above all, the edge quality you are willing to accept, so the confirmed figures for the machine you are considering are the ones stated on your quotation.
| Power Band | Mild Steel (oxygen) | Stainless Steel (nitrogen) | Aluminium (nitrogen) |
|---|---|---|---|
| 1.5 kW | Up to around 16 mm | Up to around 8 mm | Around 4-6 mm |
| 2-3 kW | Up to around 20 mm | Up to around 14 mm | Around 6-10 mm |
| 4-6 kW | Around 20-25 mm | Around 10-16 mm | Around 10-14 mm |
| 8-10 kW | Around 25-30 mm | Around 20-25 mm | Around 16-20 mm |
| 12-15 kW | Around 30-40 mm | Around 25-35 mm | Around 25-30 mm |
| 20 kW | Around 40-50 mm | Around 35-45 mm | Around 30-40 mm |
Do not specify at the top of the band – this is the mistake the table above invites. Maximum thickness is the point at which the machine will still make a cut, not the point at which it makes a good one economically. At the top of its range a laser cuts slowly, pierces slowly, is fussy about plate condition and leaves an edge that often needs work. Specify so that the thickness you cut in volume sits comfortably inside the band, and treat the maximum as your occasional-job reserve rather than your production capability.
What these machines will not cut is as important as what they will. A fiber laser is a metal process: acrylic, polycarbonate, wood, MDF, rubber, foam, glass and stone are outside it, because those materials do not absorb the 1064 nm wavelength usefully. For acrylic and other non-metal sheet, a CO2 laser is the correct machine. For heat-sensitive alloys, composites or stone, a waterjet is. If your work genuinely spans both metal and non-metal, plan two processes rather than expecting one machine to stretch.
Under the Covers
Laser Source, Cutting Head and CNC Control – What Actually Decides Performance
Machine bodies look much the same across the market. What separates one laser cutting machine from another is what is inside it, and every one of these components is specified per machine against the work it has to do – the right answer for a 3 kW panel-cutting machine is not the right answer for a 20 kW plate machine.
Three components decide how a fiber laser cutting machine performs in production: the laser source that generates the beam, the cutting head that focuses and delivers it to the material, and the CNC control that moves it along the path. A quotation that names all three in writing is a specification. One that says “imported” or “premium” without naming them is a brochure, and the difference matters more than any figure on the front page.
| Component | What It Decides | What to Specify or Ask For |
|---|---|---|
| Fiber laser source | Power, thickness reach and cut speed – and a large share of the machine price. Its wall-plug efficiency also sets your electricity cost for the machine’s whole life. | The power band in kW, the make and model in writing, the warranty term on the source itself as distinct from the machine, expected service life in operating hours, and whether that source is supported and stocked in India. |
| Cutting head | Focus quality, kerf, edge squareness, and how well one machine handles both thin sheet and thick plate. It also decides whether reflective metals are safe to cut at all. | Automatic focus or fixed focus, the head’s own power rating against the source you are buying, back-reflection protection if brass, copper or aluminium are in your mix, and how simply protective windows and nozzles are changed on the shop floor. |
| CNC controller and cutting software | How the machine pierces, leads in, handles corners, small holes and thin webs. This is where cut quality is actually won or lost, and where two machines with identical sources produce visibly different parts. | Whether it imports your DXF and DWG files directly, the nesting capability, stored cutting parameter libraries per material and thickness, and who updates the software over the machine’s life. |
| Motion system – servos, drives, guides, gantry | Positioning accuracy, repeatability, and how hard the machine can accelerate between cuts – which is what sets real cycle time on nests of small parts, not the source rating. | Positioning accuracy and repeatability as figures, rapid traverse speed and acceleration, and the drive and linear guide arrangement on each axis. |
| Chiller and cooling circuit | Whether the source holds its rated power through a full shift, and whether it keeps holding it in an Indian summer rather than at a test-bench temperature. | Chiller capacity sized against the source power and against your ambient bay temperature, plus where the rejected heat goes. |
| Frame, bed and slats | Rigidity under acceleration, and whether the machine holds its accuracy over years rather than months. A frame or gantry that flexes shows up as vibration marks on the cut edge and contour error on small features, long before it shows up on a calibration report. | How the frame is manufactured and stress-relieved before machining, the slat material, and how slats are replaced once they are cut through. |
How to Read Accuracy and Speed Figures on a Quotation
Four numbers appear on almost every laser cutting machine specification sheet, and buyers routinely compare the wrong one. Cutting speed gets the attention; acceleration usually decides the shift. Here is what each figure actually governs, together with the range commonly published across production fiber machines – so you can tell a normal figure from a remarkable one when you read a competing quotation.
| Figure | What It Governs | On Our Machines |
|---|---|---|
| Cutting accuracy | How close the head lands on the commanded point. It decides whether hole positions and overall part dimensions hold across a full sheet rather than only near the datum corner. | +/-0.03 mm. When you compare this against another quotation, check whether their figure is stated as an absolute value or per metre of travel – the two are not the same claim, and on a 6 metre bed the per-metre figure is the one that decides your part. |
| Acceleration | How hard the machine changes direction, quoted in G. On a nest of small, detailed parts this is the single biggest factor in real cycle time – the head spends most of its life speeding up and slowing down, not running at top speed. | 1 G at 1800 W, up to 1.5 G – in line with production rack-and-pinion machines, where 2-3 G is reached only on linear-motor designs at a considerably higher price |
| Maximum positioning speed | How fast the head moves between cuts. Impressive on paper and rarely reached on a real nest, because short moves never get up to speed – which is why acceleration is the more honest number to compare. | 80 m/min |
| Repeatability | How consistently the machine returns to the same point. This governs part-to-part consistency across a production run, and matters more than accuracy for anyone cutting the same component repeatedly. | Confirmed on your quotation against the configuration you specify – the range published across production fiber machines is around +/-0.02 to +/-0.05 mm |
The comparison that actually predicts your cycle time – ask both suppliers to run your own DXF file, your real nest on your real thickness, and quote a cut time for it. A machine with a lower top speed and higher acceleration will beat a faster-sounding one on small-part work, and no combination of catalogue figures will tell you that as reliably as one nest will.
The Machine Itself Is Where a Builder Earns Its Name
Components can be specified onto any machine. What cannot be bought in is the machine they are mounted to – the frame and its stress relief, the bed, the gantry and how rigid it stays under acceleration, the axis layout, the way the whole assembly is aligned and proved before it ships. That is the engineering that decides whether a machine still holds its accuracy in year five, and it is the part Sigma Mechotronics Pvt. Ltd. designs and manufactures at its own plant in Ahmedabad rather than importing as a finished unit and putting a name on it.
The machine is built, assembled and set up as a system by us, with stage inspection carried out during the build at the optical axis, framework and control stages rather than only at final test. That is also why a custom bed size, a non-standard configuration or an integration into an existing production line is an engineering conversation with the people who actually build the machine – not a variation request routed to an overseas manufacturer who may simply decline it.
On source and head selection – the fiber sources and cutting heads used across the Indian market come from a small number of established makers, and the sensible choice differs by power band, by material mix and by how the machine will be run. We specify both against your work at quotation stage and name them on the quotation, with the warranty term for each stated separately – which is exactly what you should require from any supplier, ours included.
Four Questions to Put to Any Supplier Before You Sign
01
Name the Source and Head in Writing
Not “imported” and not “premium”. The make, the model, the power rating and the warranty term for each, printed on the quotation rather than described on a call.
02
Give Me Accuracy and Repeatability as Numbers
Positioning accuracy per metre and repeatability, plus rapid traverse and acceleration. A supplier unwilling to put these on paper has told you something useful.
03
Who Installs, Commissions and Trains?
Whether the supplier’s own engineers set the machine up on your floor, tune parameters against your actual material and train your operators – or whether that is subcontracted, rushed, or billed to you afterwards.
04
Where Are the Spares Held?
Which consumables and critical spares sit in an Indian warehouse, and the honest lead time on a control board, a cutting head or a source module if one fails mid-order.
Before the Machine Arrives
What a Laser Cutting Machine Needs From Your Plant
This is the part of the purchase that gets planned last and causes the most delay at commissioning. Every item below scales with the laser source you specify, which is why utilities belong in the specification conversation rather than after the order.
| What the Installation Needs | Why It Matters and What to Check |
|---|---|
| Three-phase supply and connected load | The load scales with source power, and the chiller, extraction and compressor are additional loads on top of the machine. Confirm your incoming supply and transformer headroom before you fix the power band, not after. |
| Chiller and cooling | The laser source and the cutting head are water-cooled, and chiller duty depends on ambient temperature in the bay. Size for an Indian summer on a multi-shift day, not for an average one, and plan where the heat is rejected to. |
| Assist gas supply | Cylinders, a manifold, bulk liquid nitrogen or an on-site generator are four different economics, and the right one depends on your nitrogen volume. Getting this wrong appears later as running cost, not as a machine fault. |
| Clean, dry compressed air | Needed for air cutting and for pneumatics. Oil or moisture carried through into the head is a direct route to damaged optics, so filtration and a dryer are part of the installation rather than an optional extra. |
| Fume extraction sized for the worst material | Extraction is specified for the dirtiest thing you cut – galvanised, painted or coated stock – not the average job. On the close body machine extraction is integrated; on open type bodies it has to be designed into the layout. |
| Floor, access and staging area | A level floor, crane or forklift access over or beside the bed, and somewhere for incoming sheet and finished parts and skeleton to sit. Overhead loading only helps if there is room to stage stock next to the machine. |
| Safety zone on open type bodies | An open bed does not contain the beam in a housing, so the working area needs a demarcated, guarded zone and wavelength-rated eye protection for anyone inside it. That is floor area, and it belongs on the layout drawing from the start. |
| Nesting software and a trained operator | Cut quality and material yield are as much about programming as about the machine. Installation includes commissioning, parameter setting for your material and operator training before handover. |
Space, Weight and Electrical Load – Planning Figures
These are the figures your civil, electrical and material-handling planning has to start from. Use them to check the bay before you commit to a bed size; the exact figures for your configuration are confirmed on the quotation, because they move with power band, body type and the peripherals you specify.
| Planning Item | Figure to Work From | What It Does Not Include |
|---|---|---|
| Overall machine dimensions | From around 9200 x 3050 x 1900 mm on the smaller beds up to around 11200 x 3660 x 1900 mm on the larger ones | Chiller, extraction unit, compressor, gas manifold and control cabinet, all of which need their own positions and service access |
| Machine weight | Around 5 tonnes on a 3200 x 1600 mm machine, rising with bed size and body type | The loaded plate on the bed, which on thick heavy stock is a meaningful additional floor load |
| Working clearance around the machine | Allow access on all four sides for loading, part picking, skeleton removal, slat cleaning and service | The demarcated safety zone on open type bodies, which is additional floor area again and must be drawn in from the start |
| Connected electrical load | Budget for the laser source drawing roughly three to five times its rated output in electrical input, plus the chiller, drives, extraction and compressor on top | Your existing plant load – check transformer headroom, not just the incoming supply rating |
| Crane or forklift access | Reach over the full bed on open type machines; safe approach to the loading side on close body machines | The staging area for incoming sheet and for finished parts and skeleton, which needs its own floor space beside the machine |
The pattern we see most often – the machine is ready before the building is. Electrical work, the extraction run and the gas arrangement are the three items that hold up commissioning, and all three have lead times of their own. Ask for the utility requirements at quotation stage and start that work in parallel with manufacture – it costs nothing extra and it is the difference between cutting in the first week and cutting in the second month.
Cost
What Actually Sets the Price of a Laser Cutting Machine
There is no single price for a laser cutting machine, and a figure quoted before anyone has seen your material and part sizes is a guess dressed as a quotation. Six variables set the number, and knowing them lets you read any quote – ours or anyone else’s – properly.
| Variable | How It Moves the Price |
|---|---|
| Laser source power (1.5 kW to 20 kW) | The largest single driver, and it pulls the peripherals with it – a bigger source needs more chiller duty, more gas and more connected load, so the gap between two power bands is wider than the source price alone. |
| Bed size, standard or custom | Structure, drives, rails, gantry mass and transport all scale with the working envelope. A custom bed is engineered to your drawing rather than picked from a list, so it is priced as an engineering build. |
| Body and automation | The auto pallet changer adds a second bed, a swap drive and its guides. The close body adds cabin, interlocks, viewing window and integrated extraction. The open single pallet has none of that, which is why it is the most economical body. |
| Tube capability | A rotary attachment on a flat bed is a fraction of the cost of a dedicated chuck-fed tube machine – and does correspondingly less. Decide this on your tube volume, not on the price difference. |
| Cutting head and options | Reflective-metal rating, automatic focus, nozzle handling, and on the tube machine the +/-45 degree bevel capability. Each is specified against work you actually do, not added by default. |
| Peripherals and what the quote includes | Chiller, fume extraction, compressor, gas manifold or nitrogen generator, nesting software, installation, training and warranty. This is where two quotes most often differ without looking as if they do. |
Two quotations are only comparable when power, bed size, body, cutting head and the included peripherals are the same on both. In practice they rarely are, and the cheaper one is often cheaper because something has been left out of it – extraction, the chiller, commissioning, training, or the warranty period. Before comparing the totals, put both quotes side by side on those six lines and see what each one is actually selling you.
The second number worth working out is running cost. Electricity, assist gas and consumables – nozzles, protective windows, lenses – are paid every shift for the machine’s whole life, and on a busy machine they add up to more than the difference between two purchase prices within a few years. A source with better wall-plug efficiency, a gas supply arrangement matched to your nitrogen volume and a supplier with spares in the country are all cost decisions, not comfort decisions.
Why there is no price list on this page – a number without a specification behind it is not useful to you, and publishing one would mean either quoting the cheapest possible configuration or a range so wide it tells you nothing. Send us your material and thickness range, your largest and smallest regular part, your rough monthly volume and a drawing of the space, and you will get a specified machine with a price against that specification.
Five Steps
How to Specify the Right Laser Cutting Machine
Work through these in order. Each one narrows the specification, and taking them out of order is how buyers end up with a machine that reads well on paper and fits badly on the floor.
- 1
Decide Sheet, Tube, or Both – Honestly
This splits the range in two before anything else is discussed. Work out what share of your revenue is tube and profile work, and what share is flat sheet. Occasional tube alongside sheet is a flat bed with a pipe attachment. Tube as a product line, with welded joints needing bevelled ends, is a dedicated tube machine. If it is genuinely both at volume, it is two machines, and it is better to hear that now than after one of them disappoints.
- 2
Size the Bed Against Your Largest Regular Job
Not your average job, and not last month’s order book. Take the biggest part you would want to be able to quote for over the next few years, add clamping and nesting margin, and read that against the six standard beds. If your requirement lands between two of them, ask about a custom bed rather than defaulting upward – stepping up a size costs floor area and capital for the life of the machine.
- 3
Set Power From Thickness, Then Check It Against Volume
Write down the thickest material you must cut and the thickness you cut most of. The first sets the minimum power; the second decides whether you should go above it, because that is where cycle time turns into money. Under-specifying to protect the capital budget usually costs more in cycle time across the machine’s life than it ever saved at purchase – and unlike options, the source is not something you casually change later.
- 4
Choose the Body From Your Floor, Not the Brochure
Ask three questions. How does material get onto the bed – crane from above, or forklift from one side? How many sheet changes happen per shift, and how long is a typical programme? And who else works within sight of the machine? Overhead loading and varied stock point to an open single pallet; high sheet turnover points to the pallet changer; a shared floor, coated material or a fume-sensitive neighbour points to the close body.
- 5
Confirm Utilities and Layout Before You Sign
Connected load and transformer headroom, chiller position and heat rejection, assist gas arrangement, extraction routing, crane reach, staging area for stock and parts, and – on an open type machine – the demarcated safety zone. Get these on a drawing and start the electrical and extraction work while the machine is being built. This step decides whether you are cutting in your first week or your second month.
Avoid These Buying Mistakes
6 Mistakes Buyers Make When Choosing a Laser Cutting Machine
1
Choosing power against a budget rather than against a thickness. The budget is a number you set; the thickness is a number your customers set. A machine that cuts your main thickness too slowly costs you the saving back in cycle time every shift for years, and the source is not a component you casually swap later.
2
Sizing the bed for the orders you have instead of the ones you want. Every other specification on the machine can be discussed, upgraded or added to. The working envelope is fixed at manufacture. The first oversized enquiry you have to turn away costs more than the bed size you declined to buy.
3
Comparing two quotations that are not the same machine. Different power, different bed, different body, different head – and often a chiller, extraction, installation or training missing from one of them. Line the six price variables up on both quotes before you look at the totals.
4
Assuming a pipe attachment does the job of a tube machine. An attachment handles round, square and rectangular tube alongside your sheet work. It does not do bevel cuts, open C, H, L and I profiles, or chuck-fed throughput. Match the choice to your tube volume, not to the price gap.
5
Treating extraction, gas and cooling as things to sort out afterwards. They scale with the source, they have their own lead times, and they are the three items that hold up commissioning. Sized for the average material rather than the worst one, extraction becomes a compliance problem as well as a cost.
6
Buying the machine and forgetting who supports it. A lower price without engineers in the country, spares held in India and a real warranty is not a saving – it is a deferred cost that lands the first time the machine stops unexpectedly, and it lands during production, not during procurement.
Where They Are Used
Industries and Applications
Fiber laser cutting has become the default metal cutting process across Indian manufacturing, which is why this range turns up in almost every fabrication sector.
- Sheet Metal & General Fabrication
- Job Work & Contract Laser Cutting
- Automotive & Auto-Ancillary
- Electrical Panel & Switchgear
- Structural Steel Fabrication
- Railway & Rolling Stock Components
- Agricultural Equipment Manufacturing
- Pump, Valve & Industrial Engineering
- Elevator, Racking & Storage Systems
- Railing, Furniture & Architectural Metalwork
- Stainless Steel Kitchen & Food Equipment
- Signage & Display Fabrication
- Aerospace & Precision Components
- Tool Rooms & Maintenance Workshops
Typical flat-bed output covers the whole range of sheet and plate fabrication: brackets, mounting and base plates, machine frames, panel and enclosure blanks, gussets, gears, discs, gaskets and profile-cut components in mild and carbon steel, stainless steel and aluminium. Tube work covers frames, railings, handles, gym and furniture structures, agricultural implements and structural members, with bevelled ends where the joint is welded. The common thread is metal in flat or section form, in batch sizes from one to thousands, where the geometry changes more often than the material does.
Keeping It Running
Maintenance and Safety in Practice
A fiber laser cutting machine has far less routine maintenance than the mechanical processes it replaces, but “less” is not “none” – and on an open type body, the safety routine is the machine’s primary protection.
| Routine Task | Typical Frequency |
|---|---|
| Protective window and lens check and cleaning, nozzle inspection and replacement | Daily to weekly depending on usage – the most common cause of a sudden drop in cut quality |
| Bed slat and dross tray cleaning | Regular – build-up changes how the sheet seats and how cleanly finished parts drop |
| Rail, rack and guide lubrication | Per machine manual schedule; the dedicated tube machine has automatic lubrication on its feed system |
| Chiller water level, quality and temperature check | Regular, and always before a multi-shift run in hot weather |
| Extraction airflow and filter condition check | Regular, and sized for the worst material you cut rather than the average |
| Assist gas line, filter, dryer and pressure check | Regular – moisture or oil reaching the head damages optics |
| Guarding, interlocks, signage and eye protection audit | Regular – this is the primary protection on an open type machine |
| Full technical inspection and calibration | Annually, or under an annual maintenance contract |
Safety, in practice: the beam on these machines is invisible and hazardous to eyes at the fiber wavelength, so eye protection has to be rated for it rather than being ordinary safety glasses. On a close body machine the cabin and its interlocked doors are designed to contain the beam and to stop it firing when a door opens. An open type machine has no such housing, so the containment is procedural: a demarcated and guarded working area, rated eye protection for anyone inside it, and clear discipline about who may approach the bed while the machine is running. Interlocks and guards are never bypassed for convenience, including during setup and parameter trials – that is exactly when people are closest to the head.
Fume matters wherever coated, painted or galvanised material is cut, and extraction should be sized for the worst material in your mix rather than the most common one. Consumables in normal operation are assist gas, nozzles and protective windows; lenses and the cutting head itself are longer-life items. Where a shop has no dedicated maintenance engineer, an annual maintenance contract with our service team is usually the more economical arrangement than reacting to breakdowns.
Installation, Commissioning and Operator Training
The machine is installed and commissioned at your premises by our own technical team, aligned and proved on site, and set up with cutting parameters against the material you actually cut rather than a generic table. Your operators are then trained on the machine before handover – on your floor, on your machine, with your material and your first real jobs, not in a classroom on somebody else’s sample parts.
This matters more than buyers expect, because most problems in the first months of a new laser are operating problems rather than machine problems. A cut that has gone rough is usually a dirty protective window, a worn or off-centre nozzle, the wrong assist gas pressure, a focus that has drifted or a sheet that is not seated flat on the slats – all of which a trained operator recognises in minutes and an untrained one reports as a machine fault. Training is what converts a correctly specified machine into parts you can invoice.
What Your Operator Should Be Able to Do Before the Engineer Leaves
01
Run the Machine End to End
Start-up and shut-down in the correct sequence, load and run a nest, pause and resume safely, and stop the machine mid-cycle without damaging the head or scrapping the sheet.
02
Set the Cut for the Material
Call and adjust cutting parameters for each material and thickness, choose the right nozzle and assist gas, set focus, and know what a good pierce and a good edge look like on each metal you run.
03
Look After the Optics and Consumables
Check and change protective windows and nozzles, recognise the early signs of a contaminated window before it costs a sheet, and keep slats and the dross tray clean enough that parts seat and drop properly.
04
Work Safely and Read a Fault
Eye protection and safety zone discipline, why interlocks and guards are never bypassed even during setup, and how to read the first-line fault messages and check chiller, gas and extraction before calling for service.
Train more than one person – this is the cheapest mistake to avoid and one of the most common. Shops that train a single operator find out the cost the first time that person is on leave, resigns, or is needed on another machine, and a laser standing idle because nobody else can set it is an expensive way to learn the lesson. Put at least two people through the training, and ideally include whoever does your programming and nesting, because parameters and nesting decide cut quality as much as the machine does.
Manufacturer, Not Trader
Why Buy Your Laser Cutting Machine From Sigma Mechotronics Pvt. Ltd.
We build these machines ourselves, in Ahmedabad, and we have been building laser systems since long before fiber cutting arrived in India. That shows in how the machines are engineered and in how they are supported once they are on your floor.
Our Machine, Not a Rebadged Import
The frame, the bed and the machine structure are designed and manufactured at our own Ahmedabad plant, and the machine is assembled, aligned and proved as a system before it ships. That is why a custom bed size or an unusual configuration is an engineering conversation with the people who actually build the machine, rather than a change request routed through an overseas supplier who may decline it.
ISO 9001:2015 Certified, Inspected in Stages
A registered Indian private limited company – ISO 9001:2015 certified, MSME registered and GST registered – with stage inspection carried out at the optical axis, framework and controller stages rather than only at final test. Every purchase comes with a proper GST tax invoice under your GSTIN for input tax credit and capital equipment accounting.
2-Year Warranty, Spares Held in India, AMC Available
A 2-year warranty covers manufacturing defects in the machine body, laser delivery system, control electronics and motion system. Critical spares – lenses, cutting heads, control boards – are stocked locally rather than ordered on an international shipping cycle, and annual maintenance contracts are available once the warranty period ends.
Specification Help Before You Order
Our engineers work through your material, thickness range, part sizes and shop drawing with you before a quotation is issued – including telling you when a smaller bed or a lower power band is the right answer. Getting the specification right at this stage is cheaper for you than correcting it afterwards, and it is the part of the sale we take most seriously.
Installation, Commissioning and Operator Training
Our own technical team installs and commissions the machine at your premises, calibrates it, sets cutting parameters against your actual material rather than a generic table, and trains your operators before handover – so the machine is producing saleable parts at the end of commissioning, not weeks later.
Straight Answers
Frequently Asked Questions
The questions manufacturers and fabricators ask us most often before ordering a laser cutting machine.
It is a CNC machine tool that cuts metal by focusing a laser beam onto the workpiece to melt a narrow line through it, while a coaxial jet of assist gas blows the molten material out of the cut. On a flat-bed machine the sheet lies on a slatted bed and the cutting head travels over it on a CNC gantry; on a tube machine, chucks grip and rotate the section under the head. Because the beam is the tool, there is no punch or die and no tool change – a new part is a new program file.
Decide sheet or tube first, then let your floor decide the body. Varied job work with crane-loaded stock suits the open type single pallet; high sheet turnover on repeat batches suits the auto pallet changer; a shared floor or coated material suits the close body; occasional tube alongside sheet suits a flat bed with a pipe attachment; and tube as a product line suits the dedicated tube cutting machine. All four flat-bed configurations share the same 1.5 kW to 20 kW power band and the same six standard bed sizes, so the body choice never forces you to compromise on capability.
Mild and carbon steel, stainless steel and aluminium sheet and plate as standard, plus titanium, brass and copper where the cutting head is rated for reflective material. It will not cut acrylic, wood, MDF, rubber, foam, glass or stone – those materials do not usefully absorb the fiber wavelength, and a CO2 laser or a waterjet is the correct machine for them. If reflective metals are in your regular mix, tell us at specification stage so the head is specified with back-reflection protection.
Your thickest material sets the minimum, and your highest-volume thickness decides whether to go above it. As a broad guide, 1.5-3 kW suits thin to medium gauge sheet and lower-volume job work, 4-8 kW covers the production middle of mixed sheet and medium plate, and 10-20 kW is for thick plate and structural steel at volume. Note that extra power pays back strongly on thick plate but much less on thin gauge, where acceleration and gas dynamics become the limit rather than the source.
Size it against the largest job you want to be able to accept over the next few years, not your average job – and no, it cannot be changed later. The working envelope is fixed at manufacture, which makes it the one irreversible decision in the specification. Six standard beds are available from 3200 x 1600 mm to 6500 x 2500 mm, and if your requirement falls between two of them we manufacture custom bed sizes to a customer’s drawing rather than pushing you up a size.
Yes – a flat bed fitted with a rotary pipe and tube attachment cuts sheet and plate normally and handles round, square and rectangular tube in 3 m and 6 m lengths. What it does not do is bevel cutting, open profile sections such as C, H, L and I, or chuck-fed throughput, all of which need the dedicated tube cutting machine. Choose on your tube volume and on whether your joints need bevelled ends, not on the price difference between the two.
A fiber laser emits at around 1064 nm and a CO2 laser at 10,600 nm, and that single difference decides everything else. The shorter fiber wavelength is absorbed far better by metals including reflective ones, focuses to a much smaller spot, and is delivered through a fiber cable instead of a mirror path that needs alignment. Fiber also runs at roughly 20-30 percent wall-plug efficiency against about 5-10 percent for CO2. CO2 remains the right machine for acrylic, wood and other non-metals, which fiber cannot cut at all.
Laser gives the narrowest kerf, the squarest edge and the smallest heat-affected zone of the three, and is the fastest on thin to medium gauge metal, which is why it is chosen where edge quality and fine detail matter. Plasma cuts thick carbon steel plate at a much lower cost per cut but with a wider kerf, more heat input and edge taper, so precision parts need a secondary operation. Waterjet cuts anything at all with no heat-affected zone whatsoever, but it is slow on sheet metal and its abrasive and consumable cost per cut is high.
The source, the cutting head and the control package are specified per machine, because the sensible choice differs by power band, by material mix and by how hard the machine will be run – a 3 kW panel-cutting machine and a 20 kW plate machine are not correctly built with the same components. All of them are named on your quotation with their warranty terms stated separately from the machine warranty, and you should require exactly that from any supplier you are comparing. The machine those components sit in – frame, bed, gantry, axis layout and the assembly and alignment of the whole system – is designed and built by us in Ahmedabad.
Reflective metals – aluminium, brass and copper especially – throw part of the beam back up into the cutting head and the fiber, which can damage the head and the source. Back-reflection protection is the head and source design that safely handles that returned energy. You need it if aluminium, brass or copper appear in your work regularly rather than once a year, and it has to be specified before the machine is built rather than added afterwards. Tell us at enquiry stage which reflective metals are in your mix and at what thickness.
It earns its cost when your thickness range is wide or changes often. An automatic focus head sets focal position from the program rather than by hand, so a nest that runs 2 mm sheet and then 12 mm plate does not need an operator to stop and refocus between them – which removes both the downtime and the most common cause of an inconsistent edge. A shop cutting one narrow thickness band all day gains far less from it. Decide it from your job mix, not from the feature list.
It depends on six variables and cannot honestly be answered before they are known: laser source power, bed size, body and automation, tube capability, cutting head options, and which peripherals the quote includes. We do not publish a price list because a number without a specification behind it would either describe the cheapest possible machine or span a range wide enough to be useless. Send us your material and thickness range, your largest and smallest regular part, your approximate monthly volume and a drawing of the available space, and you will receive a specification and a price against it.
A three-phase supply with enough headroom for the source plus the chiller, extraction and compressor; cooling water via a chiller sized for your ambient temperature and shift pattern; an assist gas arrangement matched to your nitrogen volume; clean dry compressed air; fume extraction sized for the worst material you cut; a level floor with crane or forklift access and a staging area for stock; and on open type bodies, a demarcated safety zone. Ask for the utility requirements at quotation stage and start the electrical and extraction work in parallel with manufacture – those two items are the usual cause of a delayed commissioning.
Yes, provided the safety zone is treated as part of the machine rather than as an afterthought. An open bed does not contain the beam in a housing, so protection comes from a demarcated and guarded working area, eye protection rated for the fiber wavelength for anyone inside it, and clear rules about who may approach the bed while the machine runs. If your floor is shared with other trades, or the machine will sit close to workstations, the close body machine with its interlocked cabin and integrated fume extraction is the better answer.
A 2-year warranty on manufacturing defects covering the machine body, laser delivery system, control electronics and motion system. Installation and commissioning at your premises, cutting parameters set against your actual material, and operator training are all carried out by our own technical team before handover. Critical spares such as lenses, cutting heads and control boards are held in India rather than ordered on an international shipping cycle, and annual maintenance contracts are available after the warranty period.
Yes. Once the machine is installed and commissioned at your premises, our technical team trains your operators on it before handover – on your own machine and your own material, not on sample parts. The training covers running the machine end to end, setting cutting parameters, nozzle and assist gas selection, focus, changing protective windows and nozzles, daily cleaning and checks, safety discipline around the machine, and reading first-line fault messages. Put at least two people through it rather than one, and include whoever does your nesting and programming, because parameters and nesting affect cut quality as much as the machine does.
Yes. Custom bed sizes are manufactured to a customer’s drawing, because the machine is designed and built at our own Ahmedabad plant rather than imported as a finished unit and rebadged – so the frame, the bed and the axis layout can be engineered around your requirement instead of your requirement being forced onto a catalogue footprint. A custom build is worth it when your part size sits between two standard beds, when the building rather than the work sets the limit, when the machine has to fit an existing production line, or when one dominant sheet format at volume would make a purpose-sized bed pay for itself in nesting waste alone.
Far less than the mechanical processes it replaces, but the routine matters. Protective windows, lenses and nozzles are checked daily to weekly depending on usage and are the most common cause of a sudden drop in cut quality; slats and the dross tray need regular cleaning; rails and guides are lubricated to the manual’s schedule; and the chiller, extraction and gas filtration all need periodic checks. Normal running consumables are assist gas, nozzles and protective windows, with a full technical inspection annually or under an AMC.
The Full Range
Explore Each Machine From Sigma Mechotronics Pvt. Ltd.
Full specifications, sizing guidance and buying advice for each configuration, plus the rest of our fiber laser range.
Get a Laser Cutting Machine Specified for Your Work
Send us four things: your material and thickness range, your largest and smallest regular part size, roughly how many sheets or sections you cut per shift, and a drawing of the space the machine has to fit into including crane access. Our engineering team will come back with the right configuration, the right power band and the right bed – standard or custom – along with the utility requirements so you can start that work in parallel, and a quotation built against that specification rather than a catalogue.